

CAT Cable Manufacturing Plant Setup Cost 2026: Investment Analysis & Profitability
IMARC Group’s report, “CAT Cable Manufacturing Plant Project Report 2026: Industry Trends, Plant Setup, Machinery, Raw Materials, Investment Opportunities, Cost and Revenue,” offers a comprehensive guide for establishing a manufacturing plant. The CAT cable manufacturing plant setup report offers insights into the manufacturing process, financials, capital investment, expenses, ROI, and more for informed business decisions.
In addition to covering operational aspects, the report offers detailed insights into the CAT cable manufacturing plant process and project economics.
- Detailed insights into the CAT cable manufacturing plant process.
- In-depth project economics and financial metrics.
- Covers capital investments and project funding.
- Analysis of operating expenses and income projections.
- Breakdown of fixed and variable costs, direct and indirect expenses.
- Evaluation of ROI (Return on Investment) and NPV (Net Present Value).
- Profit and Loss account analysis.
- Comprehensive financial analysis for decision-making.
- Provides a roadmap for successfully establishing a CAT cable manufacturing unit.
What is a CAT Cable?
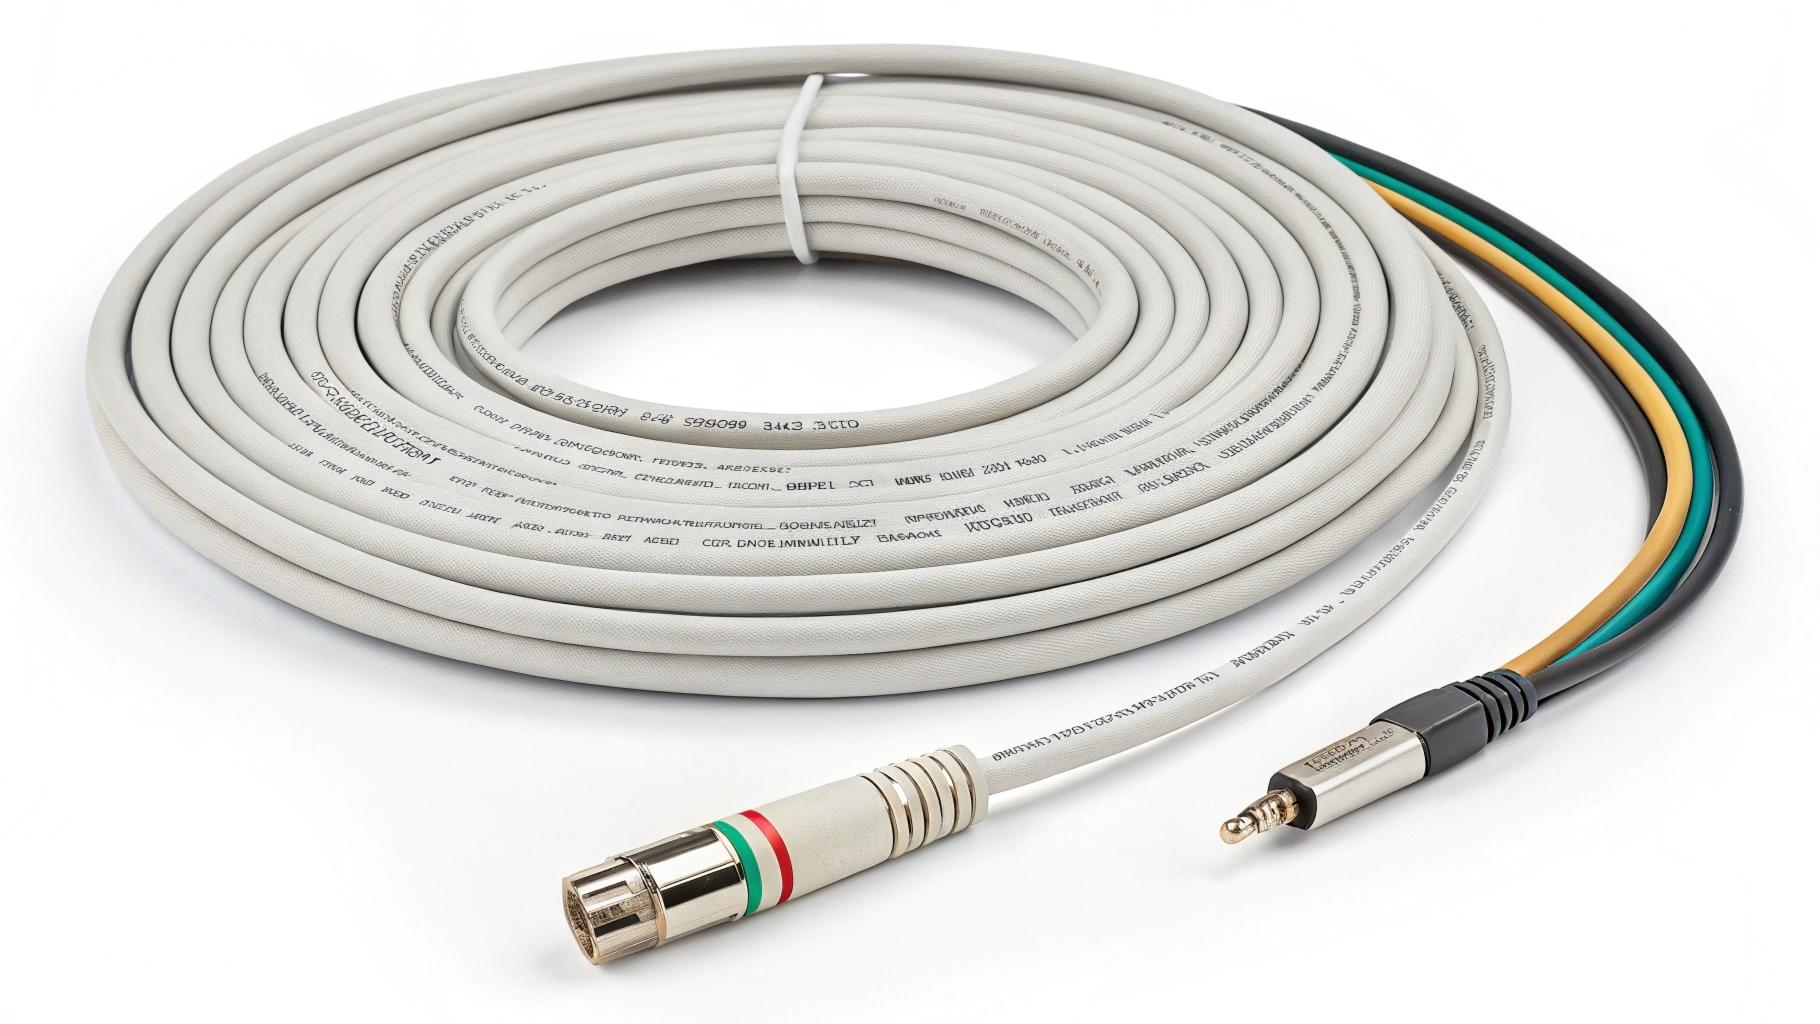
A CAT (Category) cable is a standardized twisted-pair copper cable designed for fast and reliable data transmission across LANs, WANs, telecom networks, data centres, and industrial applications. It generally consists of four pairs of insulated copper conductors twisted together to minimize electromagnetic interference, signal loss, and crosstalk. Its conductor size, insulation, twisting configuration, and overall construction are engineered to comply with international performance standards such as TIA/EIA and ISO/IEC. CAT cables are widely used in structured cabling systems to support stable and efficient communication across commercial buildings, residential infrastructure, and industrial facilities.
Market Trends and Drivers:
Common CAT cable types include Cat5e, Cat6, Cat6A, Cat7, and Cat8, each offering increasing speed and performance. For example, Cat6A supports 10 Gbps over 100 metres and is now widely used in modern installations, while Cat8 enables even higher speeds for short-distance data centre connections. Manufacturing involves processes like copper drawing, insulation, twisting, shielding, jacketing, and testing. The market is growing rapidly due to rising demand for data centres, 5G networks, smart buildings, broadband expansion, and industrial automation, along with a shift toward higher-performance and safer cable types like LSOH.
Request for a Sample Report: https://www.imarcgroup.com/cat-cable-manufacturing-plant-project-report/requestsample
Key Insights Covered in the CAT Cable Manufacturing Plant Report
Market Coverage:
- Market Trends: Analysis of current and emerging trends in the global CAT cable market across Cat5e, Cat6, Cat6A, Cat7, and Cat8 product segments and structured cabling, data centre, industrial, and broadband infrastructure end-use applications.
- Market Segmentation: Breakdown of the market by cable category (Cat5e, Cat6, Cat6A, Cat7, Cat8), shielding type (UTP, FTP, STP, S/FTP), jacket material (PVC, LSOH, TPE), conductor type (solid, stranded, CCA), form (bulk cable, patch cord), end-use application, and region.
- Regional Analysis: Distribution and performance of the CAT cable market across Asia-Pacific, North America, Europe, Middle East & Africa, and Latin America, with analysis of data centre construction pipelines, 5G rollout timelines, and broadband infrastructure investment programmes.
- Price Analysis: Evaluation of pricing trends for CAT cables by category and shielding type, reflecting copper LME price movements, polyethylene and PVC resin costs, and regional supply-demand dynamics.
- Impact of COVID-19: Examination of the effects of the COVID-19 pandemic on structured cabling supply chains, copper availability, and downstream demand from enterprise IT, data centres, and construction sectors.
- Market Forecast: Outlook and projections for the global CAT cable market through 2030, covering volume and value growth by product category, technology upgrade cycles (Cat6A and Cat8 penetration), and regional infrastructure investment-driven demand expansion.
Key Aspects Required for Setting Up a CAT Cable Manufacturing Plant
Detailed Process Flow:
- Product Overview: Comprehensive description of CAT cable products by category (Cat5e, Cat6, Cat6A, Cat7, Cat8), shielding construction (UTP — unshielded twisted pair; FTP — overall foil-shielded; S/FTP — individually shielded pairs plus overall braid), conductor diameter (AWG 22–26), insulation material (HDPE, foam-skin PE, FEP for plenum), jacket material (PVC, LSOH, PE, TPU), colour and printing specifications, and electrical performance parameters (insertion loss, NEXT, PSNEXT, return loss, propagation delay, delay skew) per TIA-568 and ISO/IEC 11801 standards.
- Unit Operations Involved: Step-by-step breakdown of all production operations: copper rod receipt and quality inspection; copper wire drawing (multi-stage wire drawing from 8 mm rod to final AWG gauge, typically AWG 23 or 24 for Cat6/Cat6A); intermediate and final annealing of drawn wire; insulation extrusion (HDPE or foam-skin PE insulation applied by single-screw extruder with precise OD control and spark tester); pair twisting (each insulated pair twisted at a precisely controlled and differentiated lay length on a pair twisting machine); cabling/stranding (four twisted pairs assembled with a central separator/spline for Cat6/Cat6A UTP or with individual pair foil shields for S/FTP variants); overall shielding application (longitudinal foil, braid, or combination for FTP/STP variants); jacket extrusion (PVC, LSOH, or TPE outer jacket by twin-screw extruder with OD control and haul-off); inkjet printing of metre marks, category designation, and manufacturer information; electrical testing (DC resistance, insulation resistance, capacitance, continuity, NEXT/FEXT attenuation by high-frequency cable analyser); and final reeling, cutting, and packaging.
- Mass Balance and Raw Material Requirements: Calculations for copper rod input per 1,000 metres of cable by AWG gauge and conductor count, insulation material (HDPE/LSOH) consumption per km, jacket compound (PVC/LSOH) consumption per km, foil and drain wire for shielded variants, rip cord and central spline quantities, reel cores and packaging material quantities, and overall copper yield from rod to finished cable.
- Quality Assurance Criteria: Standards and procedures to certify electrical performance per TIA/EIA-568-C.2 (Cat6A), ISO/IEC 11801 Ed.3 (Class EA), IEC 61156, and UL 444 standards; dimensional compliance (conductor OD, insulation OD, pair OD, cable OD); jacket material compliance (LSOH per IEC 60332, IEC 60754, EN 50267; PVC per UL 83); and compliance with RoHS Directive and REACH regulation for restricted substances in insulation and jacket compounds.
- Technical Tests: Essential electrical and mechanical tests including DC loop resistance (IEC 61196), insulation resistance, capacitance unbalance, characteristic impedance, return loss, insertion loss/attenuation, near-end crosstalk (NEXT), power sum NEXT (PSNEXT), far-end crosstalk (FEXT), equal level FEXT (ELFEXT), delay and delay skew, alien crosstalk (for Cat6A), jacket spark test, OD measurement, bend radius test, tensile strength, and LSOH/fire performance tests.
Project Details, Requirements, and Costs Involved
- Land, Location, and Site Development: Assessment of land and facility requirements for copper rod storage and wire drawing hall, insulation and jacket extrusion lines, pair twisting and cabling area, shielding application section, electrical test laboratory, finished goods warehouse, quality control room, and utilities plant, along with optimal location selection near copper rod suppliers or copper smelters, available industrial land with reliable three-phase power supply, and proximity to target markets or export logistics infrastructure, and site development cost estimation.
- Plant Layout: Design and layout planning for efficient, linear production flow from copper rod intake through wire drawing, insulation extrusion, pair twisting, cabling, shielding, jacket extrusion, printing, electrical testing, and reeling, with clearly segregated material flow lanes, cable reel movement corridors, raw material and finished goods warehousing, centralised electrical test room, and utilities (extruder cooling water, compressed air, hydraulic systems for wire drawing) in a logical and accessible arrangement.
- Machinery Requirements and Costs: Identification and capital cost assessment of all key manufacturing equipment: copper wire drawing machines (multi-wire drawing blocks for fine wire from rod); intermediate and final annealing furnaces (continuous tube or drum annealing); single-screw insulation extruders with OD control systems, spark testers, and caterpillar haul-offs; pair twisting machines (high-speed bunching or flyer twisters with lay length control); cabling or stranding machines (rigid strander or planetary strander for four-pair assembly with central separator insertion); foil shielding applicators and braid shielding machines (for FTP/STP variants); single or twin-screw jacket extruders with OD control, marking/printing systems, and spark testers; high-frequency electrical cable analysers (NEXT, attenuation, impedance measurement); reel winding and packaging lines; and laboratory test and measurement instrumentation.
- Raw Material Requirements and Costs: Determination of types and quantities of copper rod (8 mm, Grade 1 electrolytic copper per IEC 60028 or ASTM B49); HDPE, foam-skin PE, or FEP insulation compound; PVC, LSOH (halogen-free flame retardant PE/PP/EVA blend), or TPU jacket compound; aluminium-polyester foil for pair and overall shielding; tinned or bare copper drain wire and braid; polypropylene or PE central separator/spline; rip cord; reel cores; and packaging materials, along with current market prices reflecting copper LME and polymer resin prices.
- Packaging Requirements and Costs: Specifications for finished cable on wooden, metal, or cardboard reels in standard lengths (100 m, 305 m, 500 m, 1,000 m), pull-out boxes for installation-grade Cat6/Cat6A, patch cord individual poly-bag and box packaging, pallet-level stretch wrapping, and export-standard container loading configurations, including associated materials and equipment costs.
- Transportation Requirements and Costs: Logistics planning for inbound delivery of copper rod (typically by truck or rail in 2–5 tonne coil form), polymer compound pellets, and packaging materials, and outbound distribution of finished CAT cable reels and patch cords to electrical and network product distributors, ICT contractors, data centre operators, and export customers, including freight cost estimation and reel return logistics.
- Utility Requirements and Costs: Analysis of utility requirements including high-capacity three-phase electrical power for wire drawing motors, extruder drives, and annealing furnaces (a significant operating cost); process cooling water for extruder barrel and die cooling; compressed air for extruder controls and pneumatic systems; nitrogen for foam-skin PE insulation (if applicable); and associated infrastructure and running costs.
- Human Resource Requirements and Costs: Workforce planning covering wire drawing operators and maintenance technicians, extrusion process engineers and operators, pair twisting and cabling machine operators, electrical test technicians, quality control engineers (with TIA/ISO cable testing competency), compound mixing technicians, warehouse and logistics staff, sales and technical support staff for structured cabling specifiers and contractors, and plant management, along with associated salary benchmarks and training costs.
Project Economics
- Capital Investments: Initial costs for land, civil construction of wire drawing and extrusion halls, copper rod and finished goods warehouses; wire drawing machines; insulation and jacket extruder lines (a major capex item); pair twisting and cabling machines; shielding equipment; high-frequency electrical test systems; printing and reeling lines; quality laboratory; utilities; and working capital for copper rod inventory (the dominant working capital item given copper’s high unit value).
- Operating Costs: Ongoing expenses dominated by copper rod procurement (typically 60–70% of total production cost, reflecting copper’s high commodity value), polymer insulation and jacket compound, energy for wire drawing and extrusion, labour, maintenance, reel cores and packaging, and quality control consumables.
- Expenditure Projections: Year-by-year capital and operational cost forecasts, incorporating planned production volume ramp-up, copper inventory management strategy, and sensitivity to LME copper price and polymer resin price movements.
- Revenue Projections: Expected income from sale of CAT cables by product mix — Cat6 UTP bulk cable, Cat6A UTP and F/UTP bulk cable (higher margin), Cat7 and Cat8 premium cables, LSOH-jacketed variants (premium over standard PVC), and patch cords (highest value-add product) — across domestic structured cabling distributors, data centre customers, and export markets.
- Taxation and Depreciation: Analysis of applicable corporate taxes, customs duties on copper rod imports and polymer compounds, export incentives for finished cable products, and depreciation schedules for wire drawing, extrusion, and testing equipment.
- Profit Projections: Estimated profitability based on copper conversion margin (cable selling price minus copper content cost), product mix between standard Cat6 UTP and premium Cat6A/Cat7/LSOH products, production yield from copper rod to finished cable, and market pricing dynamics in target geographies.
- Financial Analysis: Comprehensive financial viability assessment including copper-price-adjusted cash flow modelling, return on investment (ROI), net present value (NPV), internal rate of return (IRR), payback period, and sensitivity analysis against copper LME price, average selling price per metre, and production capacity utilisation assumptions.
Ask Analyst for Customization: https://www.imarcgroup.com/request?type=report&id=45409&flag=C
Customization Options Available:
- Plant Location: Selection of optimal plant location considering proximity to copper rod suppliers or wire rod mills, reliable high-capacity electrical power supply, polymer compound availability, labour market for cable manufacturing, and access to target market distribution networks or export infrastructure.
- Plant Capacity: Customization based on desired annual production capacity in kilometres of finished CAT cable per year, from small focused operations (500–2,000 km/year) targeting domestic markets, to large integrated manufacturing facilities (10,000–50,000+ km/year) supplying regional and export markets across multiple product categories.
- Machinery: Choice of product range focus (Cat6 only, Cat6A and below, full Cat5e through Cat8 range), shielding capability (UTP only or full UTP/FTP/S/FTP range), patch cord manufacturing integration, level of automation (manual, semi-automatic, or fully automatic from wire drawing through reeling), and whether to include in-house copper wire drawing or to purchase pre-drawn insulated wire.
- List of Machinery Providers: Identification of suitable global and domestic suppliers for wire drawing machines, insulation and jacket extruder lines, pair twisting machines, cabling stranders, foil shielding applicators, braid shielding machines, high-frequency cable analysers, and automated reeling and packaging lines from established cable machinery manufacturers.
Key Questions Addressed in This Report:
- How has the global CAT cable market performed so far and how will it perform in the coming years?
- What is the market segmentation of the global CAT cable market by category, shielding type, jacket material, application, and region?
- What is the competitive structure of the CAT cable manufacturing industry and who are the key global and regional players?
- What is the total land area and facility footprint required for setting up a CAT cable manufacturing plant?
- What is the recommended plant layout for a CAT cable manufacturing facility from wire drawing through extrusion to testing?
- What machinery and equipment are required for wire drawing, insulation extrusion, pair twisting, cabling, shielding, jacket extrusion, and electrical testing?
- What are the copper rod and polymer compound raw material requirements and how is copper price risk managed?
- What is the estimated capital investment and operating cost for a CAT cable manufacturing plant at different capacity scales?
- What product certifications (TIA, ISO/IEC, UL) are required for commercial CAT cable sales and how long does certification take?
- And more…
How IMARC Can Help?
IMARC Group is a global management consulting firm that helps the world’s most ambitious changemakers to create a lasting impact. The company provides a comprehensive suite of market entry and expansion services. IMARC offerings include thorough market assessment, feasibility studies, company incorporation assistance, factory setup support, regulatory approvals and licensing navigation, branding, marketing and sales strategies, competitive landscape and benchmarking analyses, pricing and cost research, and procurement research.
Services:
- Plant Setup
- Factory Auditing
- Regulatory Approvals, and Licensing
- Company Incorporation
- Incubation Services
- Recruitment Services
- Marketing and Sales
Contact Us:
IMARC Group
134 N 4th St. Brooklyn, NY 11249, USA
Email: [email protected]
Tel No:(D) +91 120 433 0800
United States: (+1-201-971-6302)
